Technology for safe, efficient, and
easy-to-manage
warehouses
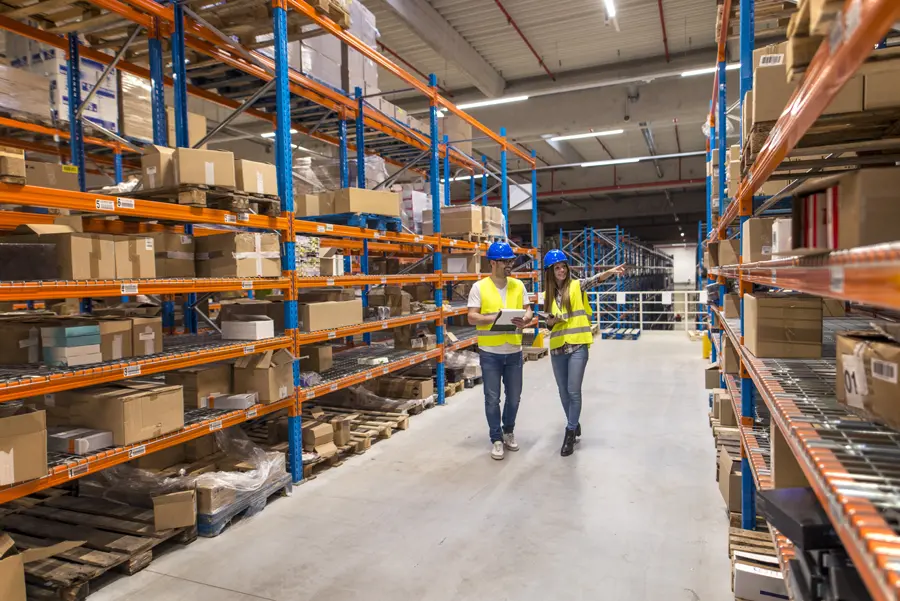
In warehousing, every product must be accurately located, securely protected, and efficiently managed. Any error or incident can result in direct financial losses.
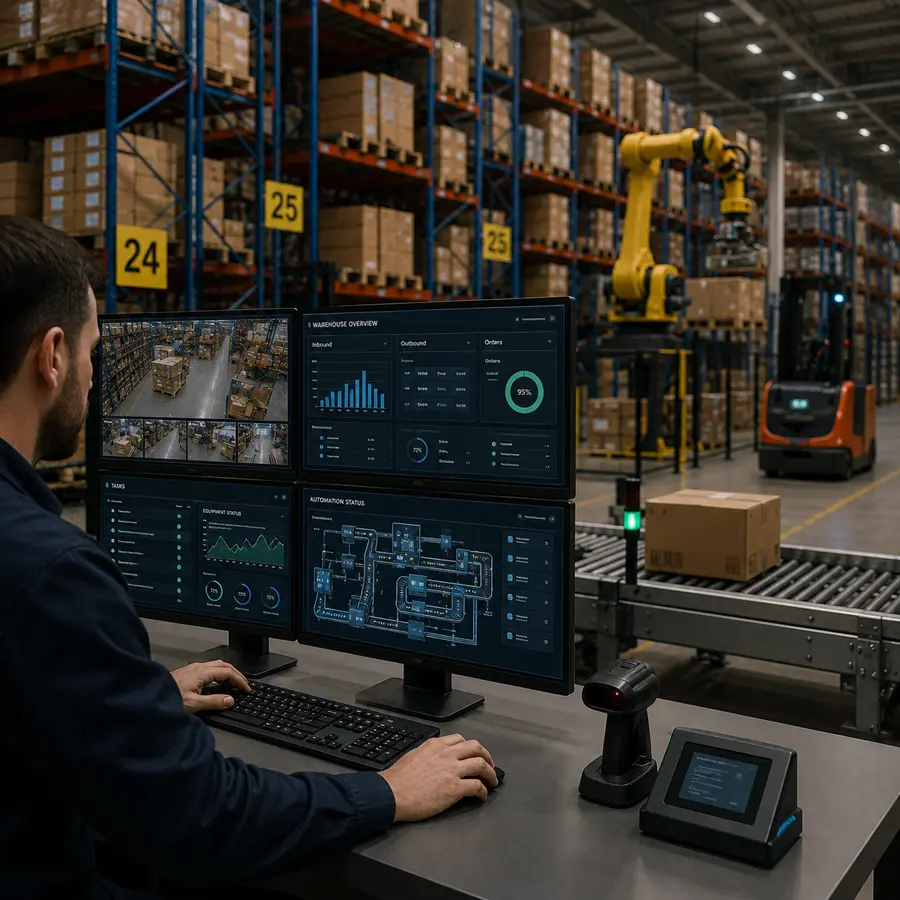
ITGlobal implements integrated solutions for warehouses and storage facilities, providing complete inventory control, enhanced security, and greater operational efficiency.
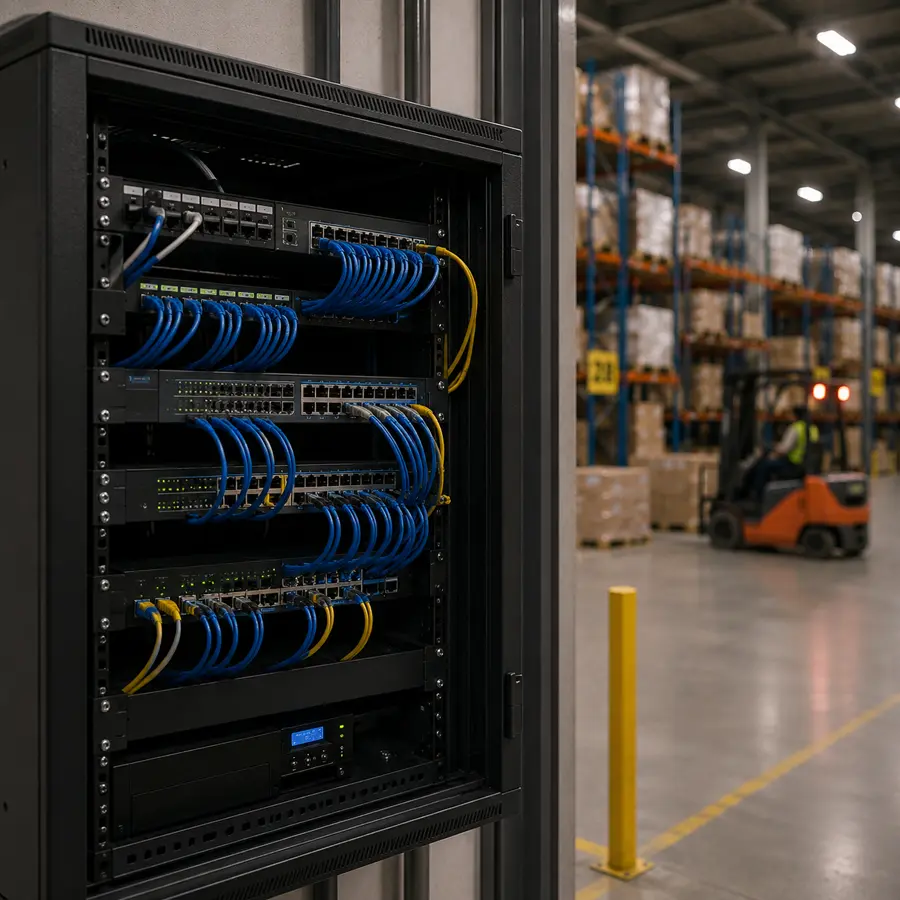
All systems are integrated into a unified infrastructure designed to deliver greater control, operational efficiency, and security.
Examples:
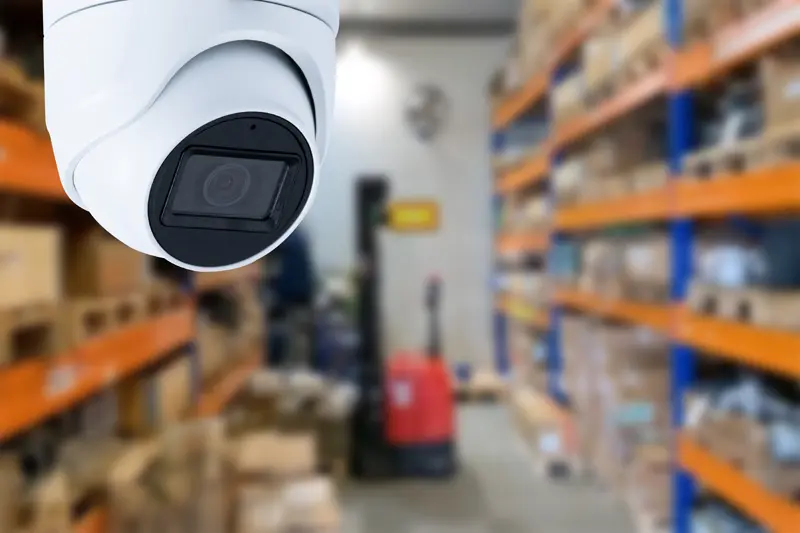
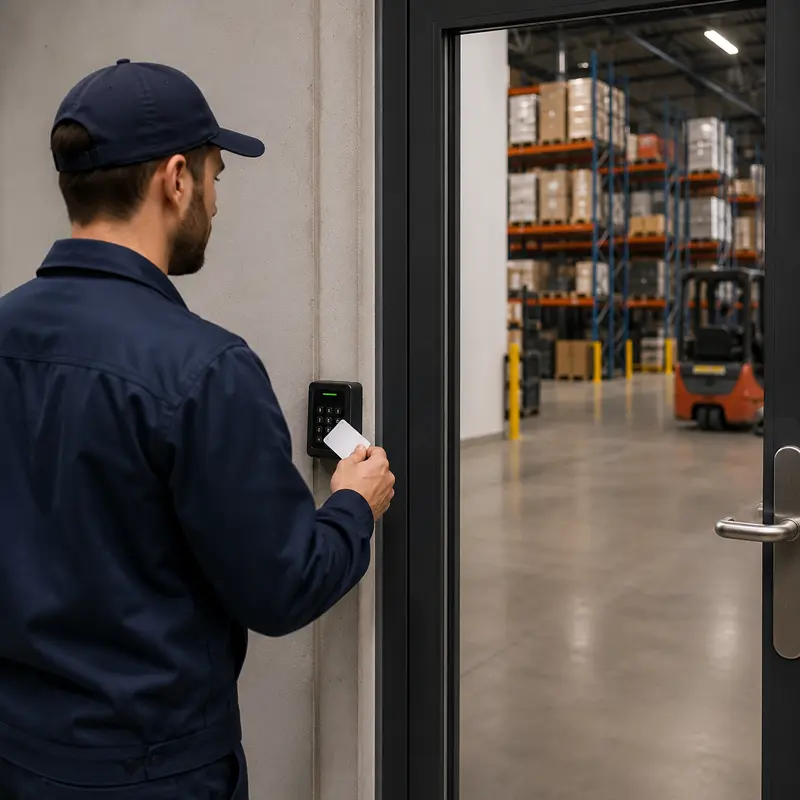
CCTV → monitors goods handling Access Control → restricts access to sensitive areas Temperature Monitoring System → automatically maintains optimal conditions
Result:
clear logistics workflows
optimized operational costs
complete control over operations
DIN
Soluții integrate pentru logistică
Why IT Global?
Extensive experience in logistics projects
Solutions tailored for warehouses and logistics centers
Complete implementation (design, installation, and maintenance)
Reliable technologies built for intensive use
Fast technical support
Want a safer and more
efficient warehouse?
Request an assessment and discover exactly where you can reduce losses and optimize your operations.
Technology infrastructure for continuous production and
operational control
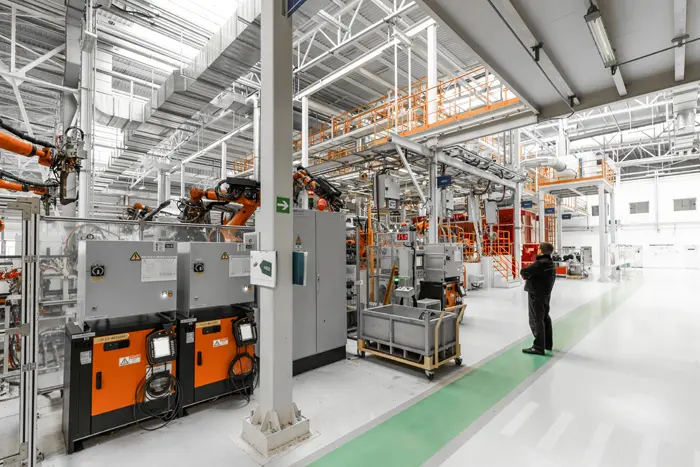
In manufacturing, every interruption comes at a cost. Lack of control, security incidents, or inefficient processes translate directly into financial losses.
ITGlobal designs and implements integrated systems for production halls and industrial facilities, ensuring security, operational continuity, and maximum efficiency.
Production Facility Challenges
→ Uncontrolled access to sensitive and technical areas
→ Increased risk of security incidents and fire
→ Limited visibility into internal operations
→ High energy and utility costs
→ Fragmented processes with no system integration
IT Global Solutions for
Manufacturing & Industrial Facilities
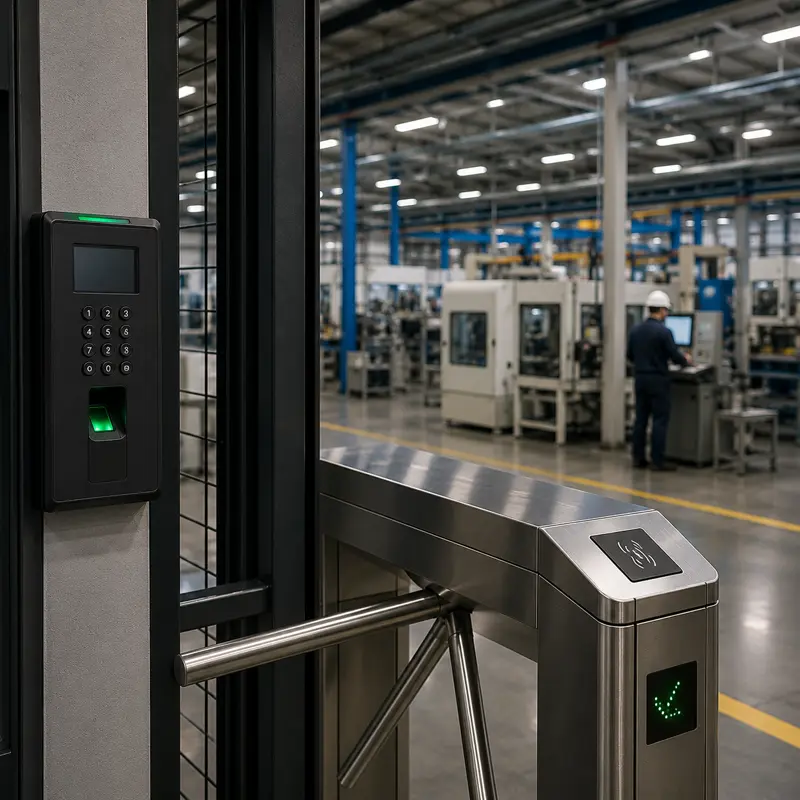
1. Industrial Access Control Systems
Strict access management for critical areas:
Role-based access for production, maintenance, and management staff
Access control for restricted areas (production lines and technical rooms)
Complete access logs and records
Integration with other security systems
Benefits:
Reduced internal security risks
Clear control over personnel access
Protection of sensitive production processes
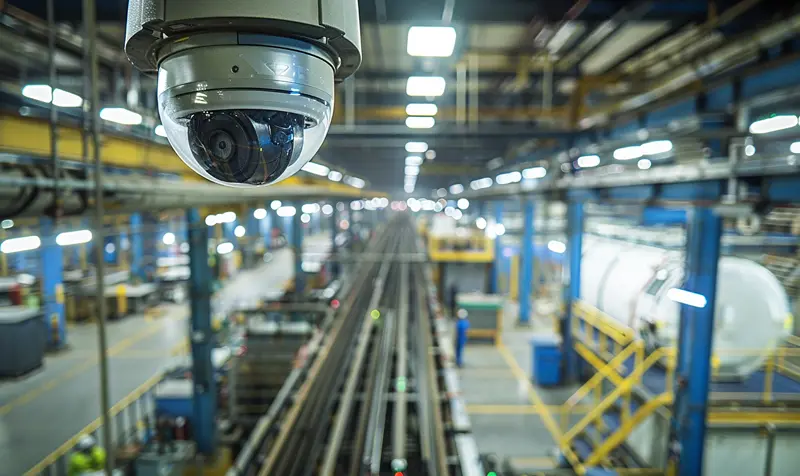
2. CCTV Video Surveillance Systems
Complete visibility into production activities:
Monitoring of production lines and logistics areas
Rugged industrial-grade cameras
Video analytics for events, workflows, and behavior
Remote access and video archiving
Benefits:
Prevention of incidents
Real-time process monitoring
Enhanced operational control
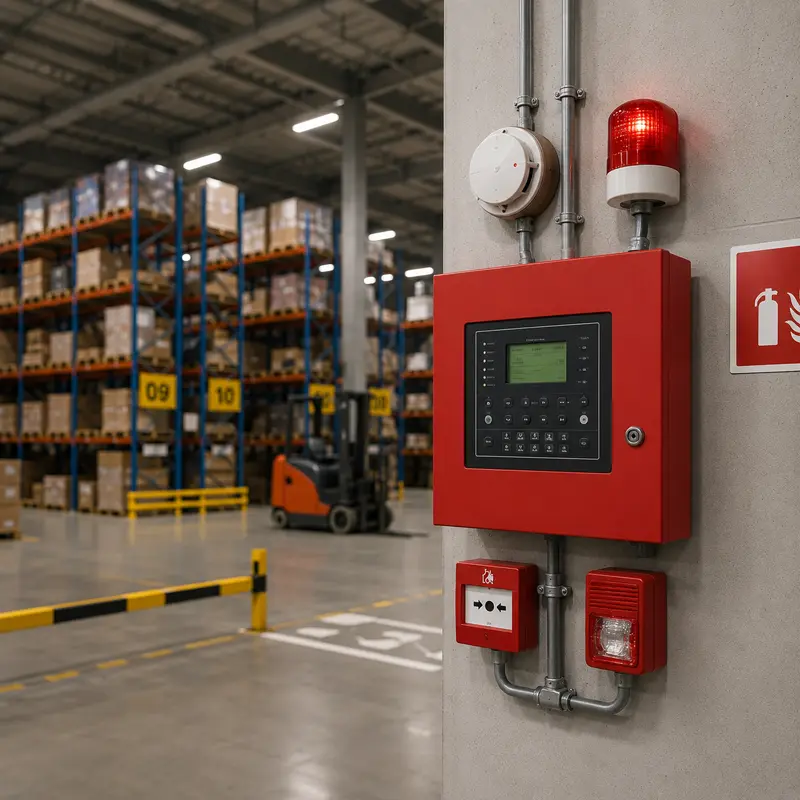
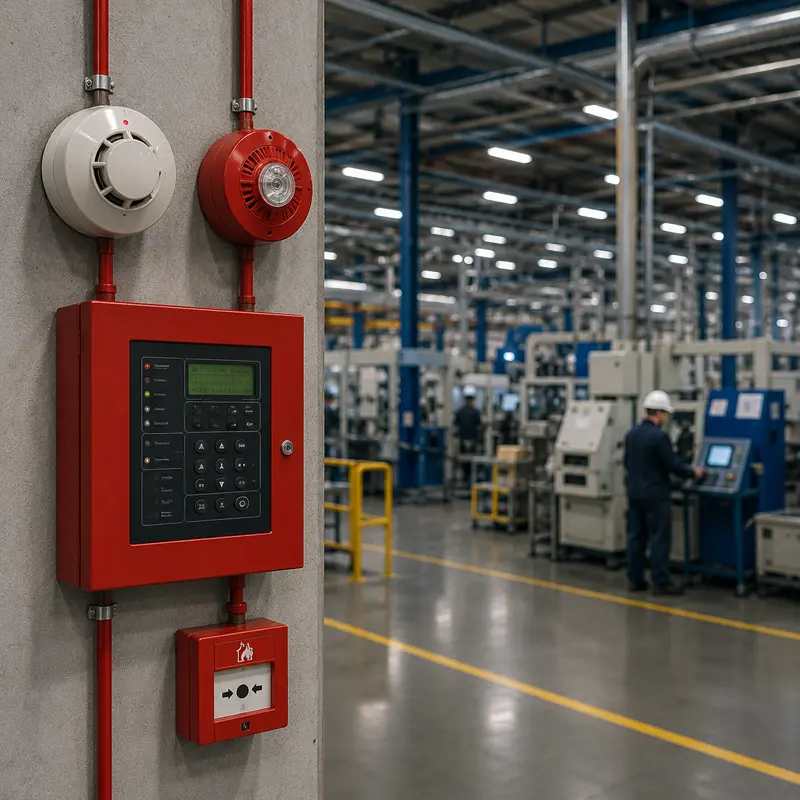
3. Fire Detection and Alarm Systems
Protection for industrial facilities:
Detectors designed for industrial environments
Addressable fire detection systems
Integration with evacuation and other safety systems
Benefits:
Reduced risk of major incidents
Protection of equipment and personnel
Rapid emergency response
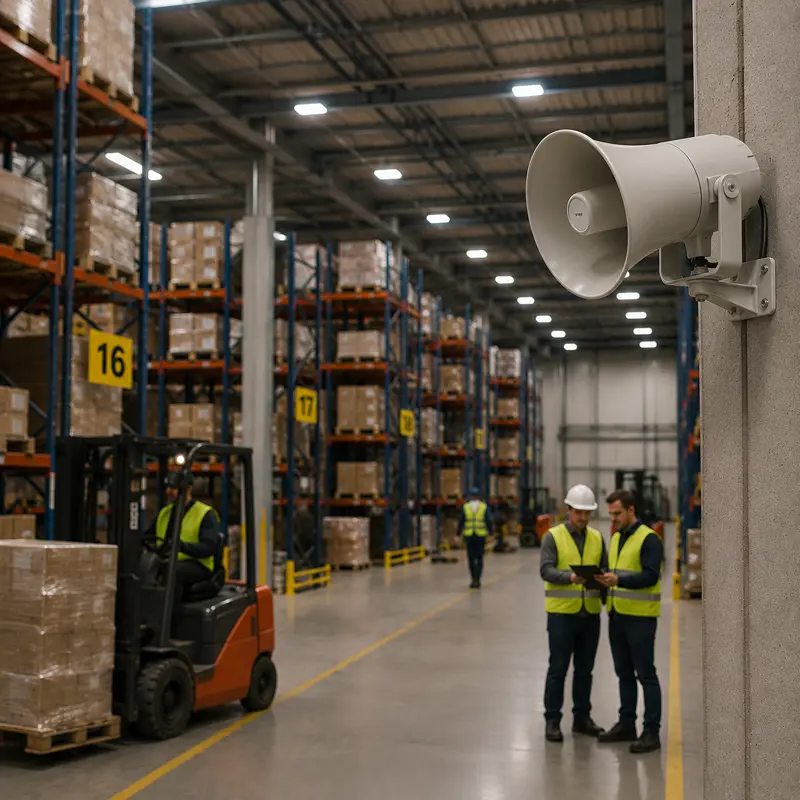
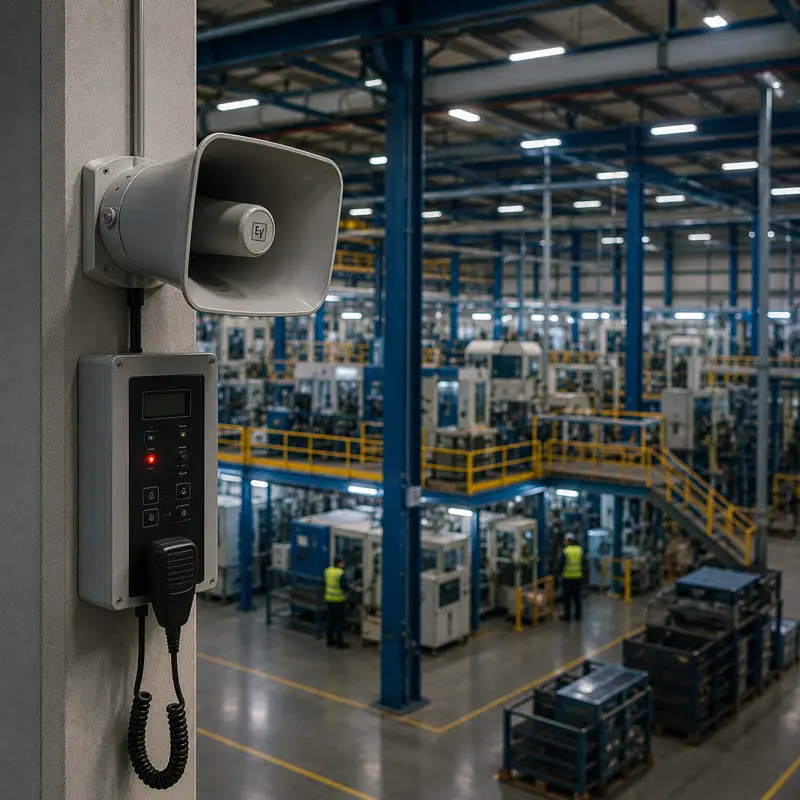
4. Public Address Systems
Fast and efficient communication:
Staff announcements
Safety messages
Critical emergency alerts
Benefits:
Better coordination across production operations
Faster response to incidents
Improved workplace safety
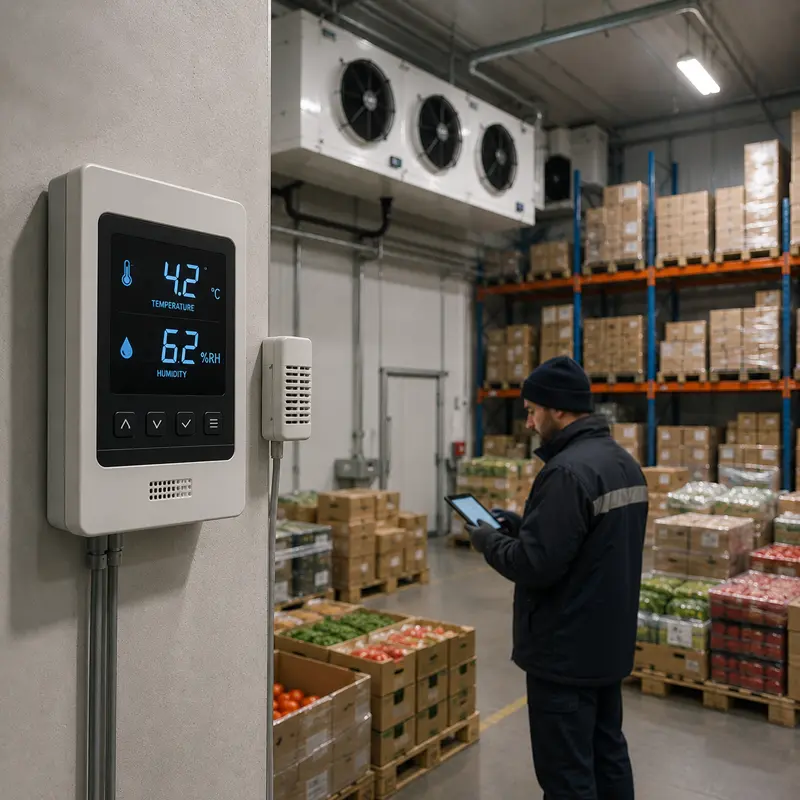
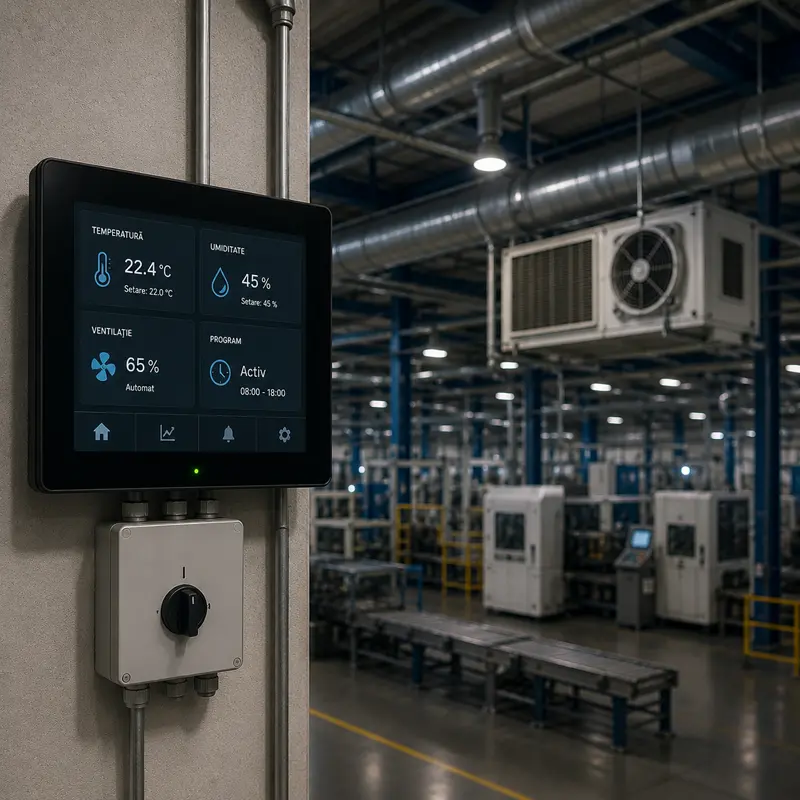
5. Intelligent Temperature and Environmental Monitoring
Maintaining optimal conditions for products and materials:
Temperature and humidity control
Continuous environmental monitoring
Automated settings based on product requirements
Benefits:
Protection of sensitive inventory
Reduced material losses
Optimized energy consumption
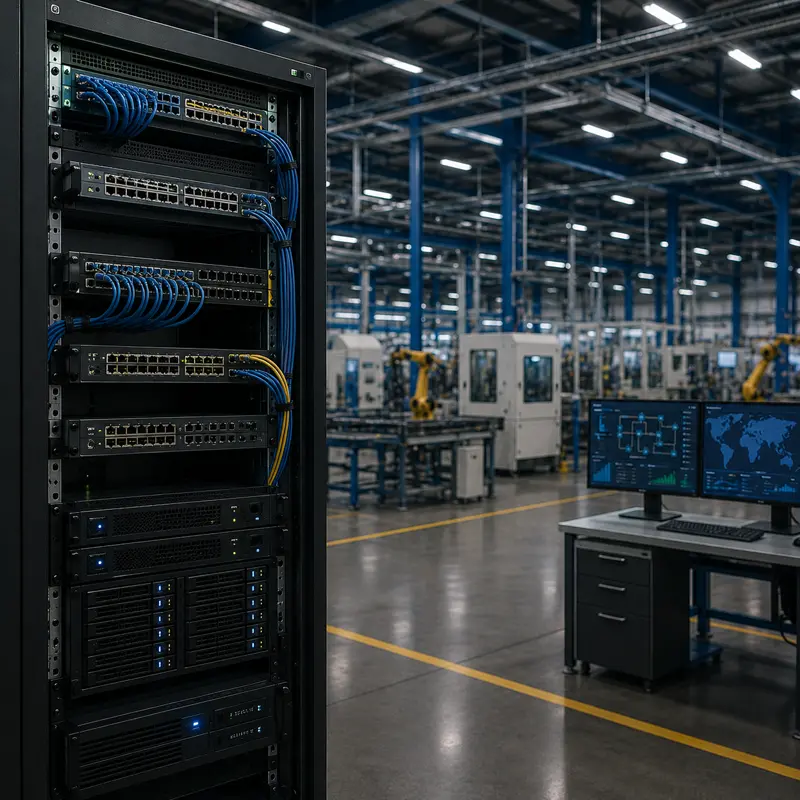
6. Network Infrastructure & IT Systems
The backbone of your operations:
Reliable networks for equipment and systems
Connectivity across production areas and facilities
All systems are designed to work together as a unified ecosystem, making them easy to manage, monitor, and optimize.
Examples:
Access Control → restricts access to critical areas CCTV → monitors production processes and verifies incidents Fire Detection System → automatically triggers safety procedures Environmental Monitoring → automatically adjusts conditions based on production requirements
Result:
streamlined processes
optimized operational costs
complete operational control
FROM
Soluții integrate pentru producție
Why IT Global?
Extensive experience in complex industrial projects
Solutions tailored to manufacturing environments
Complete implementation (design, installation, and maintenance)
Reliable technologies built for intensive use
Fast technical support
Want a safer and more
efficient
production environment?
Request an assessment and discover exactly where you can optimize costs and improve your processes.
To provide the best experience, we use technologies such as cookies to store and/or access information on your device. By consenting to these technologies, you allow us to process data such as your browsing behavior or unique identifiers on this website. Refusing or withdrawing your consent may negatively affect certain features and functionality.
Functional
Always active
The technical storage or access is strictly necessary for the legitimate purpose of enabling the use of a specific service explicitly requested by the subscriber or user, or solely for the purpose of transmitting a communication over an electronic communications network.
Preferințe
Stocarea tehnică sau accesul este necesară în scop legitim pentru stocarea preferințelor care nu sunt cerute de abonat sau utilizator.
Statistics
Stocarea tehnică sau accesul care sunt utilizate exclusiv în scopuri statistice.Technical storage or access used exclusively for anonymous statistical purposes. Without a subpoena, voluntary compliance by your Internet Service Provider, or additional records from a third party, information stored or retrieved solely for this purpose cannot generally be used to identify you.
Marketing
Technical storage or access is required to create user profiles for sending advertising or to track users across one or more websites for similar marketing purposes.